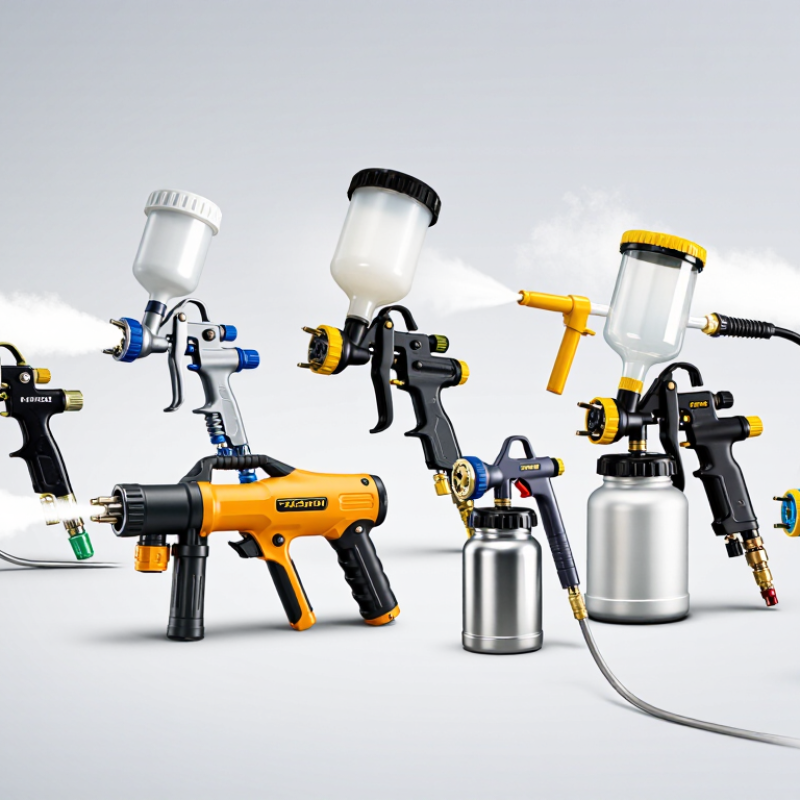
| 1 | Conventional Air Spray Gun | Compressed air breaks the coating into fine droplets. | Approximately 30–60 psi (2.1–4.1 bar) at the gun. | Produces very fine atomization and a smooth finish. Spray pattern and fluid flow are highly adjustable. | Fine finishing, furniture, general industrial coating, and small repair work. | Moderate; typically lower than HVLP because of higher overspray. | Higher overspray, air consumption, and material loss. |
| 2 | HVLP Spray Gun | High air volume at low air pressure atomizes the coating. | Air pressure at the air cap is generally limited to 10 psi or less. | Lower-velocity spray reduces bounce-back and overspray. It offers good control for detail-oriented work. | Automotive refinishing, cabinetry, furniture, trim, and maintenance painting. | High; often around 65% or higher, depending on setup and regulations. | Requires substantial air volume and may apply coatings more slowly. |
| 3 | LVLP Spray Gun | Low air volume and relatively low pressure atomize the coating. | Commonly about 15–30 psi, with lower air consumption than HVLP. | Designed for smaller compressors while retaining controlled atomization and reduced overspray. | DIY projects, automotive touch-ups, small workshops, and intermittent coating jobs. | Moderate to high, depending on nozzle, coating viscosity, and operator technique. | May spray more slowly and may struggle with very thick coatings. |
| 4 | Airless Spray Gun | A high-pressure pump forces coating through a small orifice; no atomizing air is used. | Approximately 1,000–3,000 psi (69–207 bar), depending on the coating and tip. | Very high production rate and effective coverage of large surfaces, including many high-viscosity materials. | Walls, roofs, structural steel, industrial maintenance, and large construction projects. | Moderate to high, but strongly affected by tip size, pressure, and spray technique. | More overspray and a greater risk of runs, injection injuries, and difficult cleanup. |
| 5 | Air-Assisted Airless Gun | Fluid is hydraulically pressurized, while a small amount of air refines atomization. | Fluid pressure commonly about 300–1,500 psi; atomizing air is often 5–30 psi. | Combines airless production speed with improved edge control, pattern softness, and finish quality. | Cabinetry, wood finishing, industrial metal coating, and medium-to-high production lines. | High compared with conventional air spray, when correctly adjusted. | More complex and expensive equipment with additional pressure-control requirements. |
| 6 | Electrostatic Air Spray Gun | Compressed air atomizes the coating, while an electrostatic charge attracts droplets to grounded parts. | Usually operates with conventional or reduced air-spray pressures plus high-voltage charging. | Can improve wraparound coverage and reduce material waste on conductive, suitably grounded workpieces. | Metal furniture, appliances, automotive components, and manufactured metal parts. | Potentially very high, often approximately 70–90% in suitable conditions. | Needs proper grounding, compatible coatings, controlled ventilation, and electrical safety procedures. |
| 7 | Electrostatic Airless Gun | A high-pressure fluid stream is atomized without compressed air and electrically charged for attraction. | Commonly uses airless fluid pressures from about 500–3,000 psi plus high-voltage charging. | Provides fast application and electrostatic wraparound on appropriately grounded conductive parts. | High-volume metal finishing, industrial machinery, vehicle parts, and large conductive components. | Potentially very high on properly shaped and grounded parts. | Less suitable for nonconductive substrates, recessed areas, sharp edges, or poorly grounded objects. |
| 8 | Gravity-Feed Spray Gun | Compressed air atomizes coating supplied from a cup positioned above the nozzle. | Often about 15–30 psi, depending on the gun design and coating. | Uses gravity to reduce fluid-feed pressure and waste; well suited to controlled, small-batch work. | Automotive refinishing, furniture, detail work, and small or medium repair jobs. | Generally good because little coating remains in the cup or fluid passage. | Limited cup capacity and less convenient for continuous large-area production. |
| 9 | Siphon-Feed Spray Gun | Compressed air creates a vacuum that draws coating from a container below the gun. | Usually around 30–50 psi, depending on design and material viscosity. | Simple and versatile, with a larger cup option than many gravity-feed arrangements. | General maintenance, woodworking, primers, stains, and occasional coating tasks. | Moderate; atomization is effective but air consumption and residual material can be higher. | Needs sufficient air pressure and may have difficulty feeding heavier coatings consistently. |
| 10 | Pressure-Feed Spray Gun | Compressed air or a pump pressurizes the fluid container and delivers coating to the nozzle. | Fluid pressure often ranges from 5–30 psi for air-assisted feed systems. | Supports larger fluid containers, long hoses, continuous spraying, and materials that are too heavy for siphon feed. | Large panels, industrial finishing, marine work, heavy primers, and extended production runs. | Moderate to high, depending mainly on the atomizing method and pressure settings. | Requires additional equipment and careful fluid-pressure balancing to prevent over-application. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.