| Fully Refined Paraffin Wax | Solid flakes; melting point commonly 48–68 °C; low surface moisture after cooling | Bulk density: approximately 500–650 kg/m³
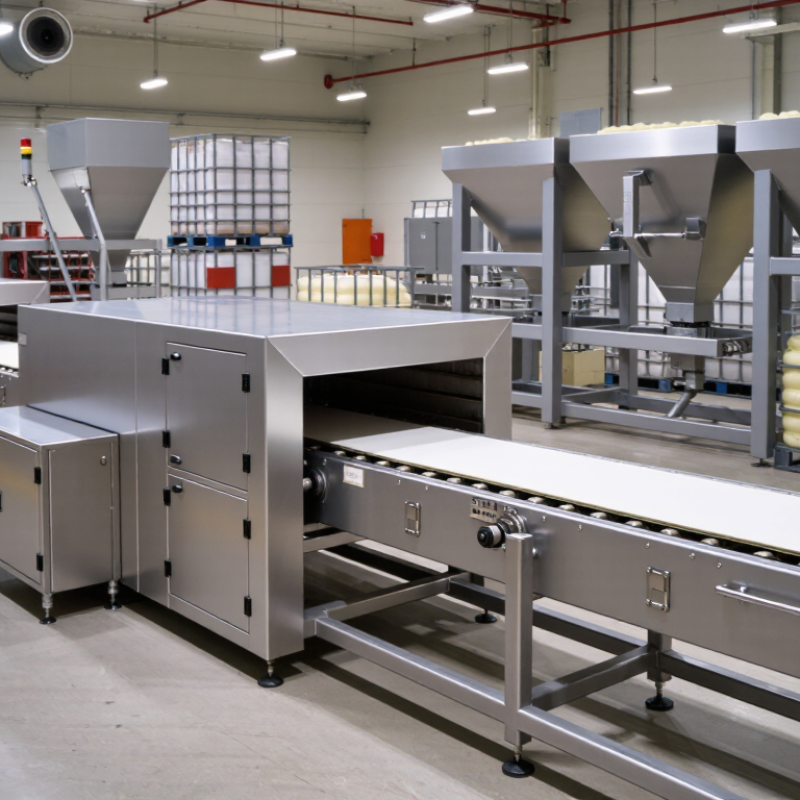
Flake thickness: 0.5–2.5 mm | Enclosed belt conveyor or food-grade modular belt conveyor | Gentle conveying helps preserve flake shape and limits dust generation during continuous production. |
| Microcrystalline Wax | More cohesive and elastic than paraffin wax; melting point commonly 60–90 °C | Bulk density: approximately 550–750 kg/m³
Potential for buildup at elevated temperatures | Low-speed belt conveyor with easy-access cleaning sections | Lower belt speed and smooth contact surfaces reduce sticking, smearing, and material accumulation. |
| Synthetic or Fischer–Tropsch Wax | Hard flakes or granules; melting point commonly 80–110 °C; comparatively high hardness | Bulk density: approximately 500–700 kg/m³
Higher impact load during transfer | Heavy-duty belt conveyor with reinforced transfer points | Impact-resistant construction helps manage hard particles and repeated loading from upstream flakers. |
| Oxidized Wax | Flakes or pellets; may contain a small amount of residual surface moisture or acidic components | Typical operating temperature: below the wax softening point
Corrosion resistance may be required | Stainless-steel conveyor with sealed bearings and covered discharge | Corrosion-resistant contact parts and enclosed conveying reduce contamination and protect the product. |
| Product Temperature | Conveyor feed temperature should remain sufficiently below the wax softening or melting point | Recommended design margin: commonly 10–20 °C below the softening point, subject to testing | Heat-resistant belt, temperature monitoring, and controlled ventilation | Maintaining a safe temperature margin reduces sticking, deformation, and belt fouling. |
| Small Production Line | Intermittent or batch operation with moderate product flow | Approximate capacity: 0.5–2 t/h
Typical conveying distance: up to 15 m | Compact flat belt conveyor with variable-speed drive | Provides flexible speed control and straightforward access for cleaning and product changeover. |
| Medium Production Line | Continuous operation with regular flake discharge from one or more cooling units | Approximate capacity: 2–8 t/h
Typical conveying distance: 15–40 m | Enclosed troughed or cleated belt conveyor with centralized tensioning | Supports stable flow over longer distances while reducing material loss and airborne wax dust. |
| Large Global Production Line | High-throughput operation with multiple shifts and limited planned downtime | Approximate capacity: 8–20 t/h or higher
Typical conveying distance: 40–100 m | Modular conveyor system with multiple drives, inspection points, and automated controls | Redundant monitoring and modular maintenance features improve uptime and simplify line expansion. |
| Inclined Conveying | Vertical elevation is required between the flaker, buffer hopper, packaging line, or storage area | Typical belt inclination: up to 15–20° for smooth flakes; steeper angles require cleats or pocket belts | Cleated belt or enclosed bucket-style conveyor | Cleats or pockets help prevent rollback and control the product layer during elevation changes. |
| Long-Distance Conveying | Material must travel through several processing or packaging zones | Recommended features: intermediate supports, belt tracking, emergency stops, and transfer chutes | Covered belt conveyor with engineered transfer stations | Proper transfer design limits product breakage, spillage, dust, and uneven loading across the belt. |
| Flake Integrity | Finished flakes must retain their shape and avoid excessive fines | Target belt speed commonly: 0.15–0.50 m/s, depending on capacity and loading width | Wide, low-speed belt with soft loading chutes | Lower speed and reduced drop height help minimize impact, abrasion, and generation of fine particles. |
| Dust and Containment | Fine wax particles may be produced during flaking, transfer, or packaging | Use enclosed covers, sealed transfer points, local extraction, and accessible dust-cleaning areas | Fully enclosed conveyor with dust extraction connections | Containment improves workplace cleanliness and helps reduce the accumulation of combustible dust. |
| Hygiene and Product Purity | Wax is used for pharmaceutical, cosmetic, food-contact, or high-purity applications | Contact surfaces should be smooth, non-porous, corrosion-resistant, and easy to inspect | Stainless-steel frame and belt components with tool-free access where practical | Cleanable construction reduces cross-contamination risks and supports documented sanitation procedures. |
| Climate and Export Conditions | Equipment may operate in humid, hot, cold, coastal, or dusty regions | Specify motor enclosure, corrosion protection, ambient temperature range, and electrical standard | Climate-adapted drive system with sealed electrical enclosures | Regional adaptation improves reliability across different humidity, temperature, and power conditions. |
| Cleaning and Changeover | Multiple wax grades or colors are processed on the same line | Consider belt access, removable scrapers, drain-free dry cleaning, and quick-release guards | Open-access or hygienic conveyor with quick-clean components | Shorter changeover times reduce production losses and lower the chance of product carryover. |
| Control and Safety | Continuous operation requires controlled material flow and rapid fault response | Include variable-frequency drive, belt-misalignment switch, pull-cord emergency stop, and overload protection | PLC-integrated conveyor with level sensors and interlocks | Automated control helps synchronize the flaker, conveyor, hopper, and packaging equipment. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.