| Working Principle | A motor-driven knife oscillates rapidly to cut sheet materials along programmed outlines. The machine normally combines cutting, creasing, marking, and drawing functions. | It enables fast, clean production of carton samples without manufacturing a metal die. | Choose a vibrating-knife system when frequent design changes, short runs, or prototype development are important. |
| Main Application | Carton prototypes, packaging samples, structural design verification, small-batch cartons, displays, inserts, and pre-production samples. | The machine is designed for flexible sample making rather than high-volume die-cut production. | Match the machine to the number of samples, material types, and carton sizes produced each month. |
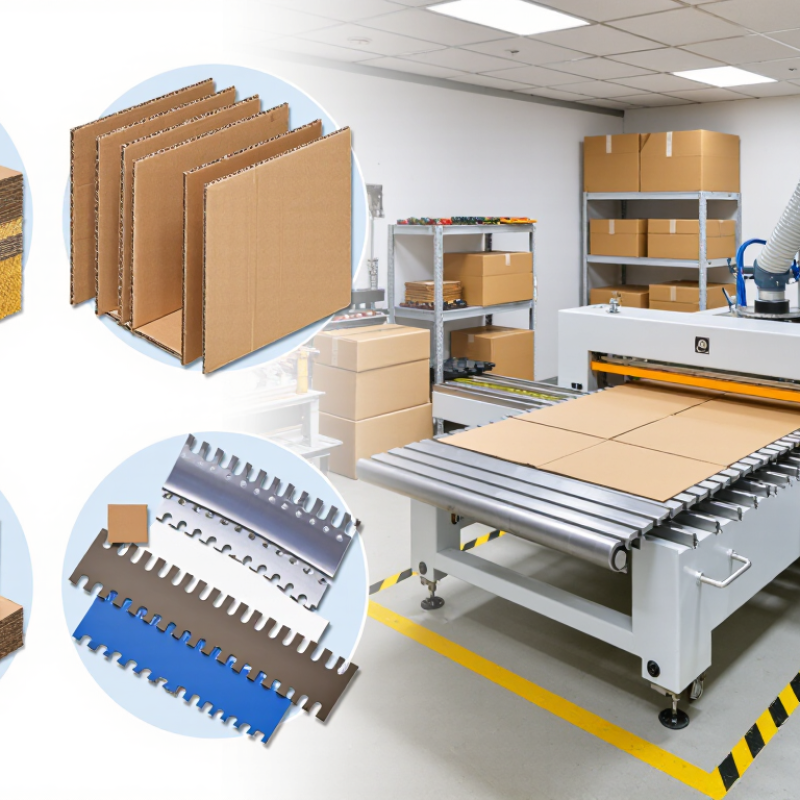
| Recommended Materials | Corrugated board, honeycomb board, paperboard, greyboard, foam board, corrugated plastic, felt, leather, and similar sheet materials. | Different materials require different knife geometries, cutting forces, and feed settings. | Confirm the machine’s approved material list and test the thickest and most difficult material before purchase. |
| Effective Cutting Thickness | Approximately 5–20 mm for many carton-proofing configurations; the actual limit depends on material density, blade type, and machine design. | A thicker or denser board may require multiple passes or a higher-force cutting head. | Select a capacity above the maximum material thickness used in your carton portfolio, not only the average thickness. |
| Working Area | Common table sizes include approximately 1,600 × 1,200 mm, 2,500 × 1,600 mm, and 3,200 × 2,000 mm. | The working area determines whether a full carton blank can be processed in one setup. | Choose a table that accommodates the largest unfolded carton blank while leaving sufficient edge clearance. |
| Cutting Speed | Typical maximum cutting speeds are about 800–1,500 mm/s, depending on the material, tool, geometry, and required finish. | Higher speed can reduce cycle time, but sharp corners and small details often require slower movement. | Prioritize stable cutting quality and acceleration control over maximum speed alone. |
| Positioning Accuracy | Many professional flatbed systems specify positioning accuracy in the range of approximately ±0.1–0.3 mm under suitable operating conditions. | Accurate positioning helps ensure that crease lines, cut lines, and printed graphics align correctly. | Ask for test results on the actual board type and sheet size used in production. |
| Tool Configuration | Common tools include an oscillating knife, drag knife, creasing wheel, plotting pen, perforation tool, and optional milling or V-cut tools. | A wider tool set allows one machine to complete more packaging operations without manual rework. | Choose the tools required for cutting, creasing, perforating, marking, and sample annotation in your workflow. |
| Creasing Performance | A powered creasing wheel or creasing tool can create fold lines in paperboard and corrugated board; tool selection must match flute direction and board structure. | Consistent creasing improves folding accuracy and reduces cracking or deformation on carton samples. | Request samples with both parallel and cross-grain creases, especially for double-wall or coated materials. |
| Material Holding Method | Vacuum tables are widely used to hold flat sheets during cutting. Zoned vacuum areas help reduce air consumption when processing smaller sheets. | Secure material holding prevents shifting, incomplete cuts, and dimensional errors. | Select a zoned vacuum table when sheet sizes vary or when thin materials are frequently processed. |
| File Compatibility | Common input formats include AI, DXF, PLT, PDF, SVG, and other vector-based formats, depending on the control software. | Compatible file import reduces preparation time and minimizes drawing conversion errors. | Verify compatibility with the design software used for structural packaging and artwork development. |
| Workflow Software | Typical functions include layer recognition, cut-and-crease assignment, nesting, contour correction, tool-path generation, and job storage. | Efficient software reduces setup time and helps operators manage repeated sample revisions. | Prefer software with editable tool parameters, preview simulation, error alerts, and simple operator controls. |
| Production Capacity | Output varies widely with carton size and complexity. A prototype can take from several seconds to several minutes, excluding file preparation and material loading. | Real productivity depends on cutting length, number of creases, tool changes, and operator handling. | Compare machines using a complete sample cycle rather than advertised cutting speed only. |
| Power Requirements | The cutting table and control system commonly require single-phase or three-phase industrial power; connected load varies by table size and vacuum system. | The available electrical supply affects installation cost and operating stability. | Confirm voltage, frequency, phase, rated power, plug type, and circuit protection requirements before installation. |
| Compressed Air Requirement | Some tool-change, pneumatic, or specialized cutting systems require a clean compressed-air supply; other configurations may not. | Air requirements influence whether an additional compressor, dryer, or filter is needed. | Request the required pressure, flow rate, air quality, and connection size for the exact configuration. |
| Safety Features | Expected features include emergency-stop buttons, protective covers or sensing systems, software travel limits, warning indicators, and controlled tool movement. | Fast-moving knives and moving gantries create mechanical hazards during operation and maintenance. | Check conformity with applicable workplace safety requirements and provide operator training before use. |
| Noise and Workplace Conditions | Noise varies with knife frequency, vacuum equipment, material type, and cutting speed. Dust extraction may be necessary for some boards and tool processes. | Noise, dust, and vibration affect operator comfort, maintenance, and the suitability of the installation area. | Evaluate the machine during a real cutting test and plan ventilation or extraction where required. |
| Machine Footprint | The total installation area is larger than the cutting table because it also includes the control cabinet, vacuum equipment, access space, and material handling area. | Insufficient clearance can restrict loading, maintenance, and safe operator movement. | Measure the complete installation zone, including front, rear, side, and service access clearances. |
| Maintenance Needs | Routine tasks include blade inspection and replacement, cleaning the table and vacuum channels, checking fasteners, lubricating specified components, and backing up software settings. | Regular maintenance supports cutting accuracy, tool life, and reliable operation. | Choose a design with accessible consumables, clear maintenance procedures, and readily available replacement tools. |
| Best-Fit Buyer Profile | Packaging design studios, carton converters, research and development departments, sample rooms, educational laboratories, and short-run packaging producers. | These users benefit from quick changeovers and the ability to produce varied designs without new dies. | Select the machine based on sample volume, board range, largest blank size, accuracy requirements, and available floor space. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.