| 1 | Verify tooling control | Mold type, cavity count, cavity balance, tool steel, venting, parting-line design, tool maintenance records, and spare-tool availability. | The factory should be able to identify each cavity, maintain cavity-to-cavity traceability, and provide preventive-maintenance intervals. For high-volume programs, a validated multi-cavity tool with balanced filling is generally more efficient than repeated single-cavity production. | ISO 3601 dimensional requirements apply to the finished O-ring, not to a specific mold design. Tooling must consistently produce the specified inside diameter, cross-section, and geometry. | Tool drawings, cavity map, first-article report, mold-maintenance log, and sample measurements by cavity. | 0–5 |
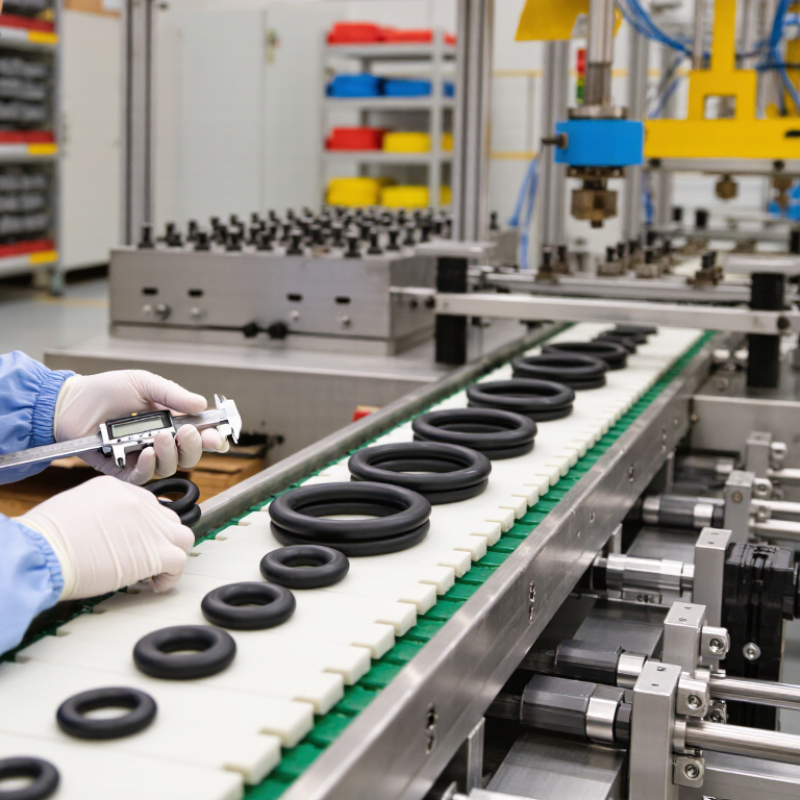
| 2 | Check dimensional capability | Inside diameter, cross-section diameter, ovality, flash, parting-line offset, and process capability indices such as Cp and Cpk. | Require a capability study using production-intent tooling and material. A common purchasing benchmark is Cpk ≥ 1.33 for critical dimensions, unless the drawing or quality agreement specifies another value. | ISO 3601-1 defines O-ring size designations and dimensional tolerances. The applicable tolerance depends on the specified size and tolerance class; it must be checked against the current standard table rather than estimated from a general percentage. | Dimensional inspection report, calibrated measuring equipment list, capability histogram, and raw measurement data from a representative production run. | 0–5 |
| 3 | Compare visual-quality controls | Flash height, burrs, surface imperfections, cracks, cuts, foreign material, flow marks, blisters, and mold contamination. | Use a documented visual standard with defined lighting, magnification, inspection distance, sampling plan, and defect limits. Critical sealing surfaces should receive stricter controls than non-functional areas. | ISO 3601-3 addresses quality acceptance criteria and relevant surface imperfections for O-rings. Visual acceptance should be agreed by defect type and severity, not described only as “good appearance.” | Approved visual master samples, defect catalogue, inspection work instruction, sampling records, and nonconformance reports. | 0–5 |
| 4 | Confirm compound and material traceability | Elastomer family, hardness, cure system, temperature range, fluid compatibility, batch identification, and certificate of analysis. | Every production lot should be traceable from finished O-rings to compound batch, mixing record, cure recipe, operator, mold, and inspection results. Hardness should be verified against the drawing or agreed specification. | ISO 3601 primarily covers O-ring dimensions, tolerances, and quality requirements. Material selection and chemical compatibility must be specified separately according to the application and relevant material standards. | Material declaration, compound batch certificate, hardness test results, mixing record, cure-curve data, and lot-traceability procedure. | 0–5 |
| 5 | Evaluate production capacity | Press size, number of molding machines, cavity count, cycle time, uptime, shift pattern, post-curing capacity, inspection throughput, and surge capacity. | Use a transparent capacity calculation: monthly capacity = machines × cavities × parts per cycle × cycles per hour × operating hours × yield. Confirm that quoted capacity includes setup, trimming, inspection, rejects, maintenance, and planned downtime. | ISO 3601 does not prescribe factory output, machine count, cycle time, or delivery capacity. Capacity should be evaluated separately while confirming that all produced parts can remain within ISO 3601 requirements. | Capacity model, machine list, historical output, on-time-delivery data, utilization records, contingency plan, and production schedule for the proposed program. | 0–5 |
| 6 | Audit inspection and calibration systems | Optical measurement, vision inspection, profile projector, force or dimensional gauges, hardness tester, temperature control, and calibration frequency. | Measurement systems should be suitable for the O-ring size and tolerance. A gauge repeatability and reproducibility study should be completed for critical measurements, with calibration traceable to recognized national or international standards. | Reliable measurement is necessary to demonstrate conformity with ISO 3601-1 dimensions and ISO 3601-3 quality criteria. ISO compliance cannot be substantiated using uncalibrated tools or undocumented visual checks. | Calibration certificates, measurement-system analysis, gauge instructions, inspection plans, control charts, and sample retention procedure. | 0–5 |
| 7 | Review quality, packaging, and change control | Incoming inspection, process controls, final release, batch segregation, packaging, shelf-life labeling, engineering-change notification, and corrective-action performance. | The supplier should provide lot-level identification, packaging that prevents deformation and contamination, defined storage conditions, documented first-article approval, and advance notification for changes to compound, tooling, process, or manufacturing location. | ISO 3601 conformity depends on controlled production and inspection. Packaging, storage, shelf life, and change control should be specified in the purchase specification and quality agreement. | Quality manual, process flow, control plan, packaging specification, traceability sample, corrective-action records, and change-control procedure. | 0–5 |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.