| Material Identity | AISI/UNS designation | Grade 430; UNS S43000; commonly designated as EN 1.4016 and JIS SUS430. | Confirm that the quoted material designation matches the drawing, end use, and applicable regional standard. |
| Chemical Composition | Main alloying elements | Chromium: approximately 16.0–18.0%; carbon: typically not more than 0.12%; manganese: typically not more than 1.00%; silicon: typically not more than 1.00%; iron: balance. | Request a heat-analysis certificate and verify the chemistry against the ordered specification. |
| Mechanical Properties | Annealed condition benchmark | Under commonly referenced ASTM A240 requirements, tensile strength is generally at least 450 MPa, yield strength at least 205 MPa, and elongation commonly at least 22% in 50 mm. Actual values depend on the adopted standard and test method. | Specify the delivery condition and require mechanical test results when forming, stamping, or bending performance is critical. |
| Physical Properties | Density and magnetic behavior | Density is approximately 7.70 g/cm³. Grade 430 is ferritic and normally magnetic in both annealed and cold-worked conditions. | Useful for weight calculations, magnetic sensor applications, appliance components, and material identification. |
| Corrosion Resistance | Service environment suitability | Good resistance in mild atmospheric, indoor, and low-corrosion environments; generally less resistant than 304 stainless steel in chloride, marine, and strongly acidic conditions. | Ask for application-specific corrosion guidance rather than selecting solely by price. |
| Common Applications | Typical end uses | Kitchen and appliance panels, automotive trim, exhaust components, decorative parts, heat-resistant indoor components, and general fabrication. | Confirm temperature, forming, surface, and corrosion requirements before approving the grade. |
| Thickness Range | Common strip thicknesses | Commercial supply commonly includes approximately 0.05–3.00 mm, subject to mill capability, temper, width, and order quantity. | State the nominal thickness, allowable tolerance, measuring method, and whether a specific standard applies. |
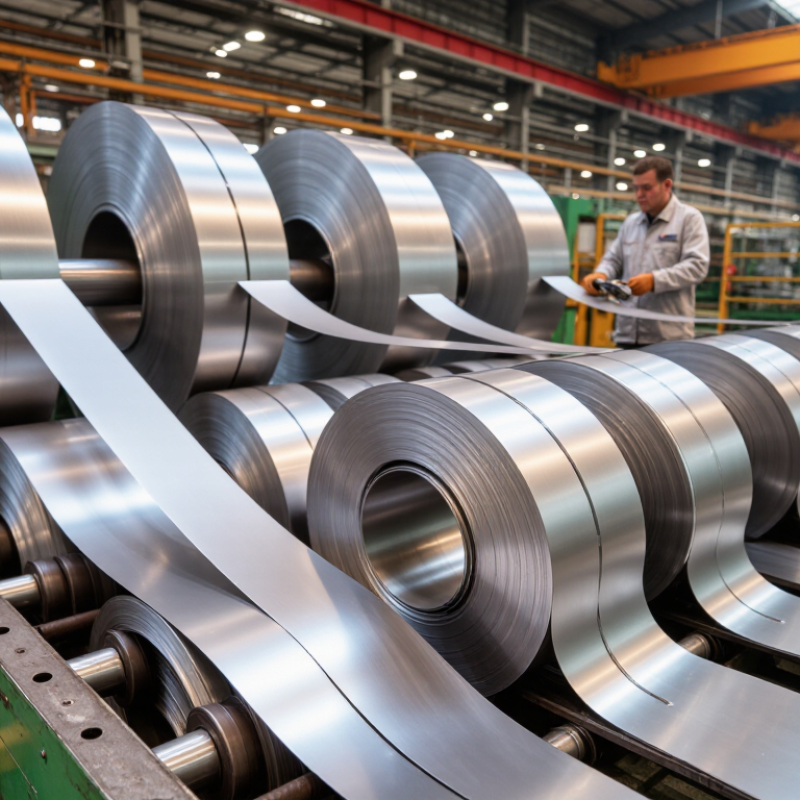
| Width Range | Slit-strip width capability | Slit widths may range from narrow precision strips below 20 mm to wide strips above 1,000 mm; the practical range depends on the processing line and required tolerance. | Provide exact width, width tolerance, edge condition, coil inside diameter, and maximum outside diameter. |
| Surface Finish | Finish and appearance | Common finishes include 2B, BA, No. 1, brushed, and polished surfaces. Finish designation, roughness, reflectivity, and protective film requirements should be stated separately. | Request a finish sample or approved reference panel for visible components. |
| Applicable Standards | Quality and dimensional standards | Common references include ASTM A240/A480, EN 10088-2, and JIS G4305. The exact standard should be agreed in the purchase order. | Avoid mixing requirements from different standards without confirming equivalent tolerances and test conditions. |
| Quality Documentation | Inspection and traceability | A complete supply package may include a material test certificate, heat number, chemical analysis, mechanical test results, dimensional inspection, surface inspection, and packing list. | Make certificate requirements part of the quotation and purchase order, not an afterthought. |
| Pricing Factor | Base stainless steel input cost | The price is affected by nickel-free ferritic alloy economics, chromium and ferroalloy costs, energy, rolling costs, and regional supply-demand conditions. | Compare quotations on the same grade, thickness, finish, tolerance, delivery term, and certification basis. |
| Pricing Factor | Processing and customization | Slitting, leveling, edge trimming, narrow-width tolerance, special hardness, brushing, polishing, protective film, and custom packaging increase processing cost. | Request a line-item quotation so material cost and conversion charges can be evaluated separately. |
| Pricing Factor | Order quantity and minimum order quantity | Larger, repeatable orders generally reduce setup and slitting costs per kilogram; small trial orders may carry setup, sample, or minimum-order charges. | Ask for tiered pricing at sample, trial, and annual-volume levels. |
| Pricing Factor | Logistics and trade terms | Freight, insurance, export documentation, duties, customs clearance, inland delivery, packaging, and currency exchange can materially change the landed cost. | Compare total landed cost under the same Incoterms, destination, currency, and delivery schedule. |
| Supplier Screening | Manufacturing and processing capability | Verify access to annealing, pickling or cleaning, cold rolling, slitting, edge control, surface inspection, and dimensional testing appropriate to the order. | Capability should be validated with equipment information, sample data, and recent inspection records. |
| Purchasing Step 1 | Prepare a technical specification | Define grade, standard, thickness, width, tolerances, finish, temper, edge condition, coil dimensions, quantity, packaging, and certificate requirements. | A complete specification prevents non-comparable quotations and costly rework. |
| Purchasing Step 2 | Request and normalize quotations | Request pricing, production lead time, sample policy, minimum order quantity, payment terms, trade terms, validity period, and included inspection documents. | Use one standardized request-for-quotation form for every candidate supplier. |
| Purchasing Step 3 | Approve samples | Check thickness, width, burr height, flatness, surface defects, finish consistency, coil condition, and forming performance against the approved specification. | Do not approve production solely from photographs or a certificate without physical sample review when appearance is important. |
| Purchasing Step 4 | Issue a controlled purchase order | Include the agreed standard, revision, tolerances, inspection plan, packaging instructions, delivery term, claim procedure, and required documentation. | The purchase order should take priority over informal messages or verbal specifications. |
| Purchasing Step 5 | Pre-shipment and receiving inspection | Review coil labels, heat numbers, certificates, packaging condition, quantity, dimensions, surface quality, and any agreed third-party inspection report. | Maintain traceability from the received coil to the production batch and final product. |
| Supplier Selection Priority | Recommended scoring balance | A practical evaluation can assign approximately 30% to quality compliance, 25% to total landed cost, 20% to delivery reliability, 15% to processing capability, and 10% to service and documentation. | Adjust the weighting according to application risk, volume, and the cost of material failure. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.