| Material Grades | ASTM A36 EN 10025 S235JR JIS G3101 SS400 | Grade must match the buyer's design code, mechanical requirements, welding procedure, and destination-market regulations. | Review the mill test certificate, heat number, chemical composition, yield strength, tensile strength, and elongation. | Provide a grade cross-reference table while confirming that equivalent grades are not automatically interchangeable without engineering approval. |
| Thickness | Common commercial range: 0.5–25 mm; exact availability depends on grade, width, rolling method, and mill capability. | Specify nominal thickness, permitted tolerance, cut-to-length requirement, and whether the material is classified as sheet or plate for the project. | Check thickness measurements at multiple points and compare them with the applicable product standard and purchase order. | Offer a thickness-tolerance confirmation before production and provide inspection records for every production lot. |
| Width and Length | Typical stock widths: 1,000–2,000 mm; common cut lengths: 2,000–6,000 mm, subject to equipment and order quantity. | Confirm maximum coil or sheet dimensions, cutting accuracy, allowable camber, squareness, and edge condition. | Review the dimensional inspection report, packing list, and photographs of markings and finished bundles. | Support custom cut-to-length orders, nesting suggestions, and dimensional approval drawings when required. |
| Surface Condition | Hot-rolled, pickled and oiled, cold-rolled, or blasted surface depending on the application. | Define acceptable scale, rust, pits, scratches, oiling condition, and surface preparation level before ordering. | Use approved samples, visual inspection under suitable lighting, and surface-condition requirements written into the contract. | Send pre-shipment surface photographs and explain whether minor mill marks are permitted by the applicable standard. |
| Mechanical Properties | Values vary by grade and standard. For example, ASTM A36 commonly specifies a minimum yield strength of 250 MPa and tensile strength of 400–550 MPa. | Mechanical properties must be suitable for forming, structural loading, machining, or welding requirements. | Confirm test direction, test temperature where applicable, sampling method, and results on the material test certificate. | Arrange third-party inspection or witnessed testing when required by the contract, project owner, or financial institution. |
| Chemical Composition | Carbon, manganese, silicon, phosphorus, sulfur, and other elements must comply with the selected grade standard. | Low-carbon chemistry may be preferred for improved weldability; the final requirement should follow the approved grade and welding procedure. | Compare heat-analysis results with the specified standard and verify the heat number on the sheet, bundle, and certificate. | Provide traceability from raw material heat to finished bundle and notify the buyer before any approved substitution. |
| Quality Inspection | Inspection may include dimensions, appearance, chemistry, tensile testing, bend testing, and quantity verification. | Inspection scope should be agreed before production, especially for structural, pressure-related, or safety-critical applications. | Accept mill certificates, inspection reports, loading photographs, quantity records, and independent inspection reports where applicable. | Maintain a documented nonconformity process with corrective action, replacement, credit, or rework options. |
| Packaging | Export bundles commonly use steel straps, protective wrapping, edge protection, waterproof paper or plastic, and pallets when suitable. | Packaging must prevent movement, moisture damage, edge deformation, and corrosion during inland transport and ocean shipment. | Approve bundle weight, lifting points, package dimensions, shipping marks, moisture protection, and container-loading photographs. | Adapt packaging to container limits, crane handling, destination climate, and buyer requirements for galvanized or coated protection. |
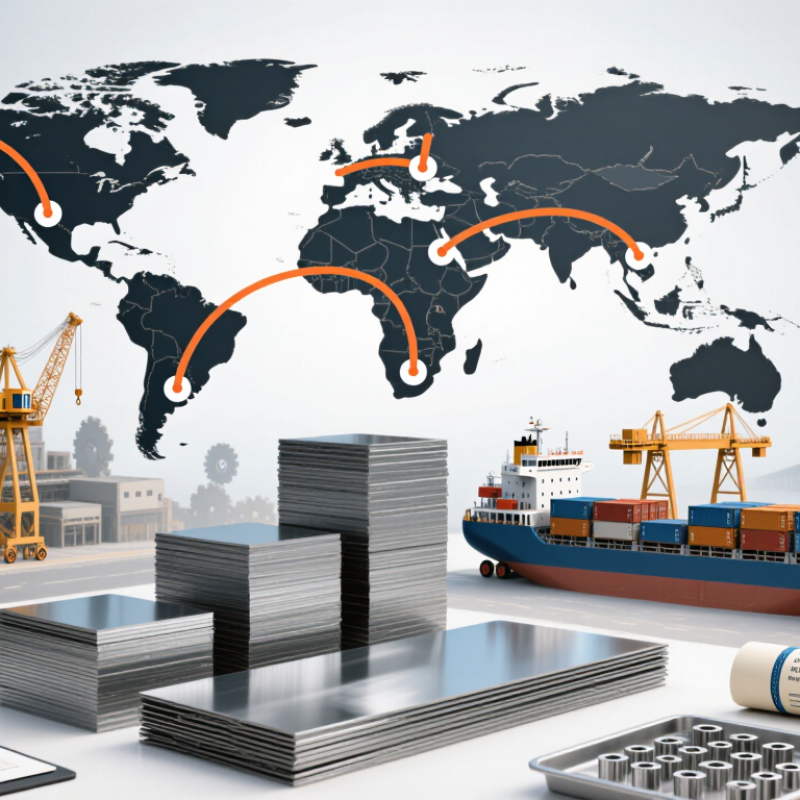
| Shipping and Incoterms | Common terms include EXW, FOB, CFR, CIF, and DAP. Ocean freight is generally preferred for full-container or bulk orders. | Define the named place or port, cargo insurance responsibility, export customs responsibility, and risk-transfer point. | Verify commercial invoice, packing list, bill of lading, certificate of origin, insurance certificate when applicable, and export declaration. | Provide freight quotations, booking updates, container-loading records, estimated sailing information, and document dispatch tracking. |
| Indicative Transit Planning | Production and preparation commonly require about 2–6 weeks; ocean transit often requires about 2–8 weeks, depending on route and port congestion. | Build a schedule that includes order confirmation, production, inspection, port handling, customs clearance, and local delivery. | Use a milestone schedule with confirmed production date, inspection date, vessel information, estimated arrival, and document date. | Report delays promptly and offer revised schedules, alternative routing, or partial shipment assessment when feasible. |
| Order Quantity | Small trial orders may be available from several tonnes; full-container and bulk orders normally provide better freight efficiency. | Calculate required net weight, bundle weight, container payload, cutting loss, and safety stock before final confirmation. | Compare pro forma invoice, packing list, weighbridge records, and bill of lading quantity. | Support trial orders, repeat-order specifications, mixed-size loading plans, and consolidated shipment evaluation. |
| Payment and Contract Terms | Common structures include a deposit with balance against shipping documents, letter of credit, or other mutually agreed trade terms. | Payment milestones should correspond to technical approval, production completion, inspection, and shipment documentation. | Confirm product description, grade, quantity, tolerance, delivery term, inspection clause, claim period, and applicable law in writing. | Provide a clear quotation validity period, transparent surcharges, bank-detail verification, and change-control procedure. |
| Traceability and Marking | Bundle marking normally includes grade, dimensions, heat number, batch number, quantity, weight, and destination marks. | Markings must remain legible throughout loading, unloading, storage, and fabrication. | Match physical markings with the material certificate, packing list, purchase order, and inspection report. | Use durable labels and provide digital records that allow each bundle to be traced back to its production heat. |
| Storage and Corrosion Guidance | Store sheets indoors or under a waterproof cover with ventilation, drainage, separators, and protection from condensation. | Storage instructions should reflect local humidity, coastal exposure, storage duration, and whether the surface is oiled. | Check packaging integrity on arrival and record visible corrosion, wet packaging, dents, or handling damage before unloading. | Provide receiving, storage, and claim-reporting guidance, including recommended photo and evidence requirements. |
| After-Sales Support | Support should cover technical questions, document corrections, shortage or damage claims, and replacement assessment. | Agree on response time, claim evidence, inspection method, remedy options, and communication channels before shipment. | Maintain a complete claim file containing order number, bundle number, photographs, measurements, certificates, and delivery records. | Assign a dedicated contact for international orders and provide written corrective-action updates until the issue is closed. |
 © Copyright 2020 Tianjin Tanghaidongyang Valve Co., Ltd. All Rights Reserved.